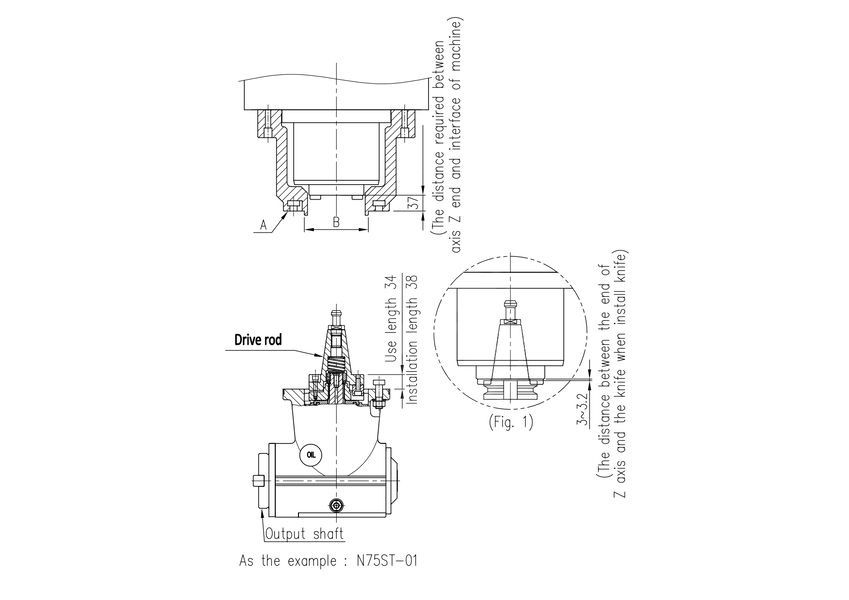
- The use length is 34 mm, the assembly length is 38 mm, and please check the distance between the end of axis Z and the interface of the machine after the holder, the distance between the end of axis Z and the interface of the machine must be 34 mm; the head bearings and parts will be damaged if the distance is over 34 mm.
- Please check parallelism of plane A on holder with precision gauge, and make sure it must be in 0.01 mm (the can't exceed 0.02mm). The height error of the head rolling to the center of each angle’s output shaft will be influenced by tolerance of plane A larger.
- The concentricity tolerance of outer B and Z axis of main axis also must be in 0.01 mm definitely. (the can't exceed 0.02mm).
- The height error of the head rolling to the center of each angle’s output shaft and various precision will be influenced by tolerance bigger of parallelism of plane A and concentricity tolerance of outer B; worse still the noise, rub & buzz, and damage of bearings and parts will be caused when the head rolling.
- When install knife (as fig. 1), the distance between the end of Z axis and the knife should be 3 ~ 3.2 mm, drive rod of head will press down if the distance longer, and cause the damage of head bearings and parts.
- NEVER knock the head body when correct the precision of right angle, and the problem caused by error installation and use is not covered under warranty.
In order to keeps the spindle bearing and gear to lubricate if the milling head haven’t use more than three month form deliver date or stop use more than three month. Please according to keep milling head as following:
- Before connect the milling head, please turn upon the spindle more than five times. That in order to make bearing and gear moistens lubricant oil.
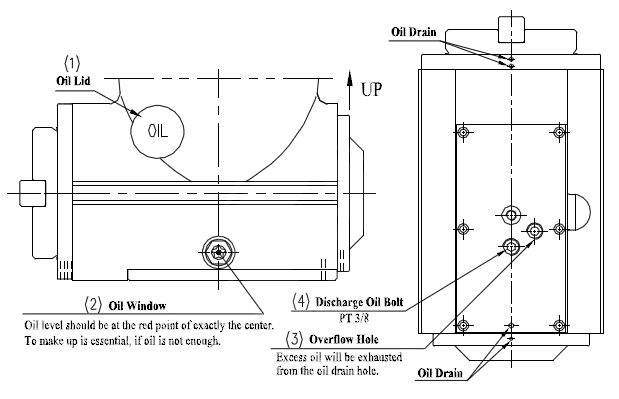
- Oil must be checked each time before using. Add more hydraulic oil (ISO-68 or ISO-AW32、hydraulic oil #10)when necessary, oil level as the drawing shown.
- Excess oil will be exhausted from the oil drain hole (location as the drawing shown). Excess oil will scavenge the lubricating grease to cause is for the bearing of the main spindle damage. But oil shortage will make the gear life short. So, keep correct oil level and never make oil higher than the red point at the center on the oil window.
- Open the oil lid to check and make sure that oil is circulating during operation.
- The reduction ratio is 1:1
- This milling head’s main spindle only Right Turn use. Can not reverse turn use. Only when use for tapping working.
- This milling head is designed for vertical use or keeping stock only.
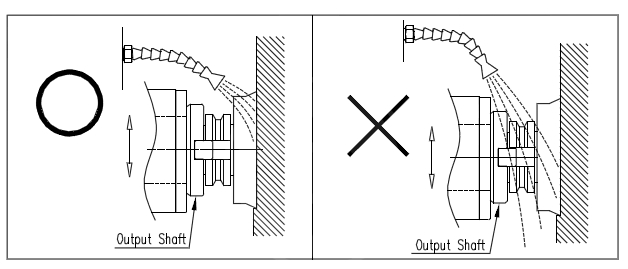
- When using cutting fluid during milling operations, properly adjust the coolant spray method and never spray or flush cutting fluid directly onto the milling head spindle. Because the spindle rotates during milling, a rotational clearance naturally exists between the spindle and the head housing. Under the direct impact of a pressurized coolant stream, the internal oil seals cannot guarantee complete prevention of coolant ingress. Therefore, it is recommended to use an air-mist cooling valve (air/water mixture) or a 6.3 mm low-pressure fluid stream with an adjustable coolant hose for easy nozzle positioning. Ensure that coolant nozzles are directed specifically at the cutting zone between the milling cutter and workpiece—never flush directly against the milling head body or spindle—to safeguard and maximize the service life of the milling head.
- ISO-68 or ISO-AW32、HYDRAULIC OIL #10 is applied by this milling head. The same or identical hydraulic oil should be always used.
- Check oil level to be sure it at the red point of the oil level center, not more, before using each time under normal condition.
- Under normal operation condition, it is necessary to change lubricating oil for the gear transmission system every 3 months or 250-300 hours. The oil lids is located as (1) and the location of the oil discharge hole is as (2). Turn off the discharge oil bolt for discharging the oil and changing new one.
PS: This milling head hasn’t add oil, please add oil to the red point of the oil level center by milling head install finish.
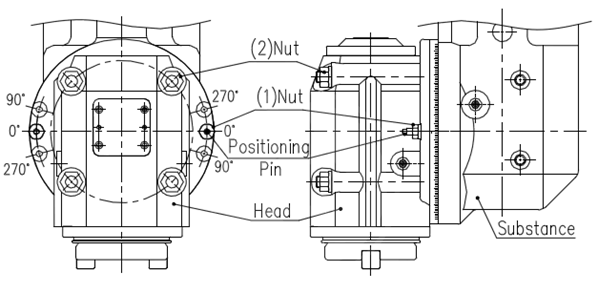
This head has 2 positioning pins at 0°、90°、270° (Diagonal direction), please follow the steps below to operate when need to position at 3 angles above:
- Locking nut (1), and remove positioning pin. (Loosen the nut (1), and the positioning pin can be knocked tight.)
- Loosen nut (2). (The angle can be rotated with just loosening a little bit, and do NOT remove the nut.)
- Rotating the head to the angle desired of processing.
- Move back positioning pins and press tightly by hand, and lock a little bit the nut (2) to be fit with machine, then knock tightly with tool, and lock tightly nut (2). (Please lock tightly with diagonal way.) (About 25kgf-m.)
PS:
- Please remove the foreign body or dirt completely in the hole when using positioning pin, and the positioning precision will be influenced by the foreign body or dirt in the hole.
- Positioning pin have to plug in the correct hole site, or will make the bad machining accuracy.
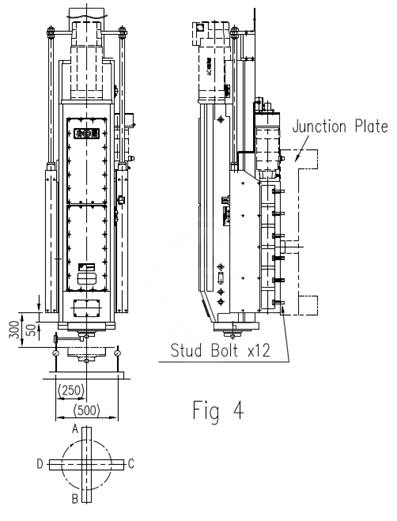
After fixing the sliding seat on the heavy duty double column milling machine, put the milling head body downward to descend 50 mm. Place a surveying indicator on a bed plate (level datum plane) to start correcting precision. First, place the surveying indicating needle on the surface of the spindle and touch the bed plate with the indicator. Note, the reading on the indicator should be back to zero. Then rotate the spindle with a hand and read the figures at A. B. C. D on the indicator, as Fig 4. A and B are left and right correcting points. The readings at the two points should be the same when correcting. Loosen the 12 bolts on the sliding seat (as shown on Fig 4) and adjust, if needed, until reaching the needed value, then screw up the bolts tightly. C and D are front and rear correcting points. The reading on these points should be adjusted, according to working situation. Second, put the head body downward and descend it until 300 mm. Then correct it by following the previous way. It can be used after completing the correcting positions.
For keeping the normal function of milling head to work with the biggest efficiency, and extending the use-life, ordinarily we must make a thorough maintenance, the staff and operators must maintain the machine actually according to the warning as follows:
- After stopping work every day, must clean iron bits on cutter head, and clean up the head completely each 4 weeks, and give the lubricant oil to all the sliding face appeared, and turn off the power.
- Before starting the machine every day, please check oil, and supply enough oil if the oil is insufficient according to the required.
- Please stop the machine immediately if there are abnormal condition of main spindle overheat, abnormal vibration, abnormal noise, and inform the relative staff, and continue to work after removing the trouble.
- Please release the lubricant oil polluted and clean the oil tank when the lubricant oil is polluted, and pour in new lubricant oil anew.
- The lubrication of sliding seat is lubricated by hand-shake oiler, and supply the lubricant oil before working every day.
- Interior lubrication of milling head should be changed once 3 months.
- Main spindle bearing’s gap must be adjusted depends on the requirement.
- The gap between head and sliding seat must be adjusted depend on the requirement.
- Please check the connector of electric wire once a year at least, for avoiding slack or corrupt.
- Please push the speed change lever to the position of high speed for lubricating main spindle’s precise bearing, and rotate the main spindle with hand, let main spindle rotating over 5 times when you want to use it if you haven’t use this machine 3 months or over 3 months since delivery date, or you interrupt the use time about/over 3 months. You should maintain the machine according the procedure mentioned above each 3 months after delivering the machine.